Polymaker PolyCast Natural PVB 1,75mm, 750kg
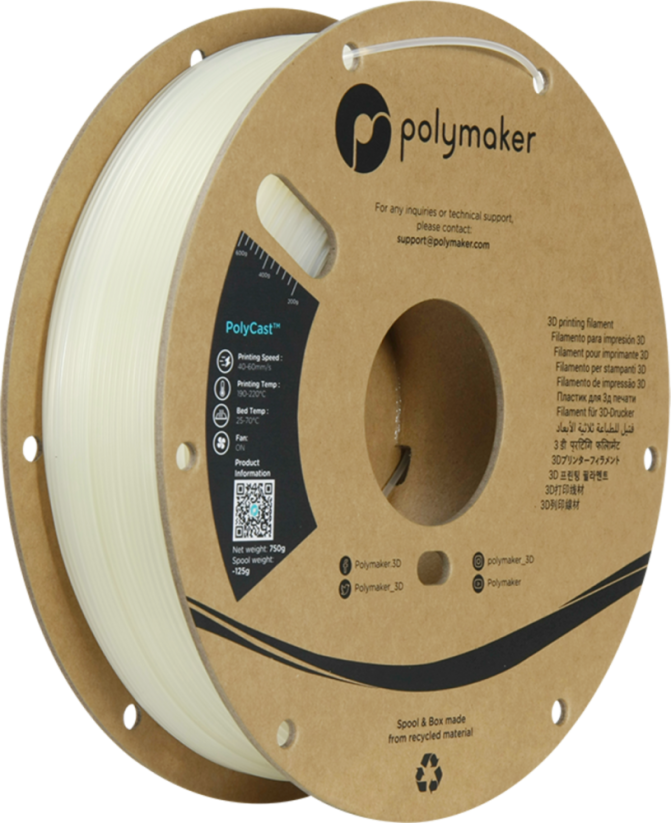


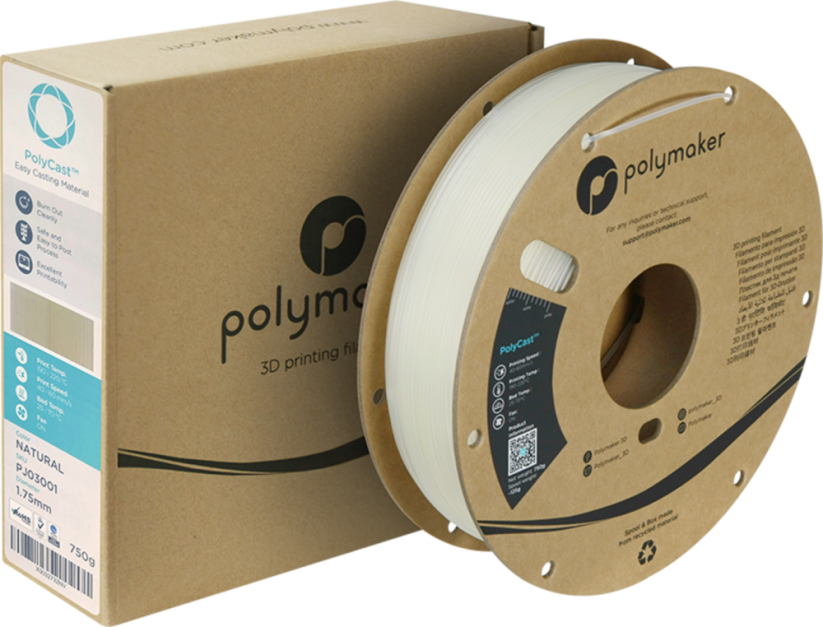


Polymaker PolyCast Natural PVB 1,75mm, 750kg

Polymaker PolyCast is a specialized PVB filament for investment metal casting using the lost-wax method - ideal for jewelry, dental technology, and precision castings.
✔️ PVB material with low ash content - residue-free burnout in the mold
✔️ Chemical smoothing with isopropyl alcohol (IPA) vapors
✔️ Print temperature 190-220 °C, bed 25-70 °C
✔️ Easy printability comparable to PLA, minimal warping
✔️ Tensile strength 37.5 MPa, tensile modulus 1745 MPa
✔️ Suitable for jewelry making, dental technology, and mechanical prototypes
✔️ Compatible with gypsum investment materials for lost-wax casting
✔️ Recommended dry storage (silica gel), drying 45 °C / 6-8 h Show more
Polymaker PolyCast is a specialized PVB filament for investment metal casting using the lost-wax method - ideal for jewelry, dental technology, and precision castings.
✔️ PVB material with low ash content - residue-free burnout in the mold
✔️ Chemical smoothing with isopropyl alcohol (IPA) vapors
✔️ Print temperature 190-220 °C, bed 25-70 °C
✔️ Easy printability comparable to PLA, minimal warping
✔️ Tensile strength 37.5 MPa, tensile modulus 1745 MPa
✔️ Suitable for jewelry making, dental technology, and mechanical prototypes
✔️ Compatible with gypsum investment materials for lost-wax casting
✔️ Recommended dry storage (silica gel), drying 45 °C / 6-8 h Show more
Polymaker PolyCast is a specialized PVB filament designed for investment (precision) metal casting using the lost-wax method. After printing, the model can be smoothed with isopropyl alcohol (IPA) vapors and then burned out of the mold without residue, creating a precise cavity for the cast metal. The material is an ideal choice for jewelers, dental technicians, and mechanical prototype casters.
Key features
PolyCast belongs to the family of PVB materials with low ash content, which means it leaves no residue in the casting mold after burnout that would compromise the quality of the cast. It prints easily, with good bed adhesion and minimal tendency to warp. The model surface can be smoothed with IPA vapors, achieving a smooth glossy finish without visible layer lines - crucial for cast jewelry and precision mechanical parts.
The material combines ease of printability comparable to PLA, chemical smoothing capability, and clean ash-free burnout. Mechanically, it offers a tensile strength of around 37.5 MPa and a tensile modulus of 1745 MPa, sufficient for handling models prior to the casting process itself.
Printing parameters
| Parameter | Value |
|---|---|
| Material | PVB (polyvinyl butyral) |
| Nozzle temperature | 190-220 °C |
| Bed temperature | 25-70 °C |
| Print speed | 40-60 mm/s |
| Recommended layer height | 0.1-0.2 mm |
| Fan speed | 50-100 % |
| Vicat softening | 67 °C |
| Tensile strength | 37.5 MPa |
| Tensile modulus | 1745 MPa |
| Flexural strength | 60.2 MPa |
| Impact strength (unnotched) | 9.6 kJ/m² |
| Enclosure / heated chamber | Not required |
| Drying before printing | 45 °C / 6-8 h (if moist) |
Who is Polymaker PolyCast Natural PVB suitable for
PolyCast is intended primarily for:
- jewelers producing rings, pendants, and other jewelry using the lost-wax method
- dental laboratories for casting crowns, bridges, and inlays
- engineering and design workshops for casting small-series metal parts
- modelers and artists needing decorative castings
- users who want to take advantage of IPA chemical smoothing to achieve a smooth surface without sanding-based postprocessing
Thanks to its low ash content, the material is compatible with standard gypsum investment materials for investment casting.
Printing tips
- Store the filament in a dry environment (ideally in a sealed box with silica gel) - PVB is hygroscopic.
- If moisture is absorbed, dry the filament at 45 °C for 6-8 hours.
- To smooth the model, place the print in a sealed container with IPA (isopropyl alcohol) vapors - the liquid must not directly touch the model.
- Smoothing time ranges from 30 minutes to several hours depending on the desired level of smoothness.
- Use a nozzle diameter of 0.4 mm or smaller to achieve fine details, which are critical for casting models.
- For small jewelry models, print with a low layer height (0.05-0.1 mm) and lower speed (30-40 mm/s).
- The bed can be printed on cold, but slight heating to 40-60 °C improves the first layer.
- Do not use retraction longer than 5 mm - PVB tends to produce fine stringing, which is removed during smoothing.
Detailed information on other materials can be found in the categories PLA, PETG, ABS, and ASA.
Dianchang Road, Bixi Street No. 15, Building C and B 215513 Changshu City, Suzhou City, Jiangsu Province China
inquiry@polymaker.com