Filament Spectrum PA6 CF15 1.75mm BLACK 0.75kg
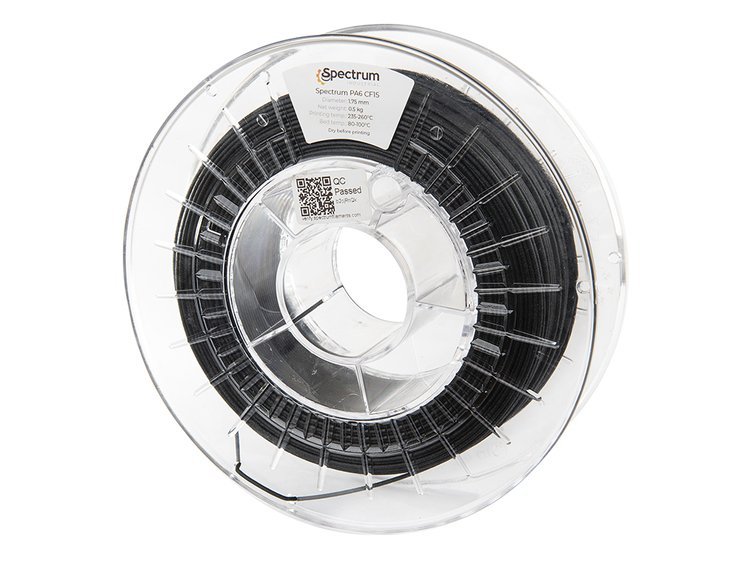
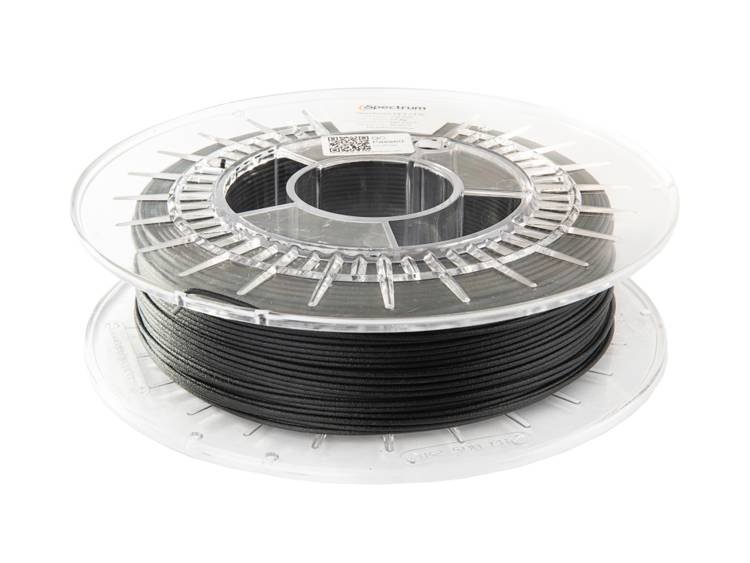
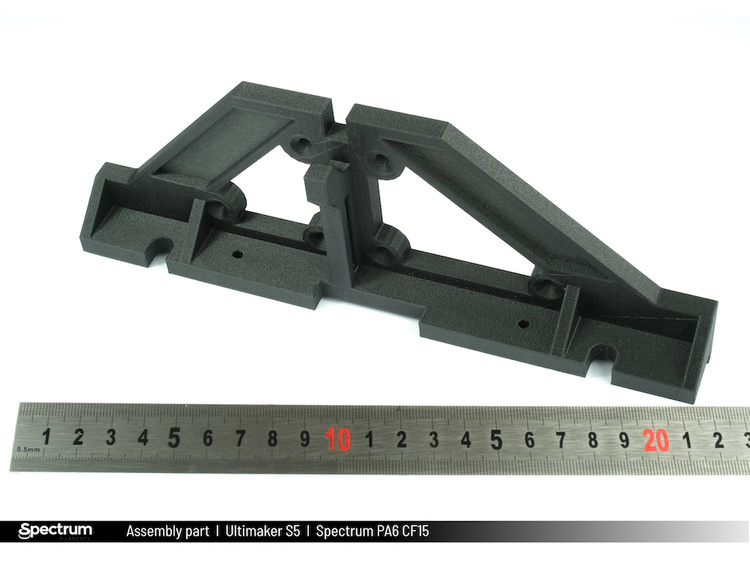
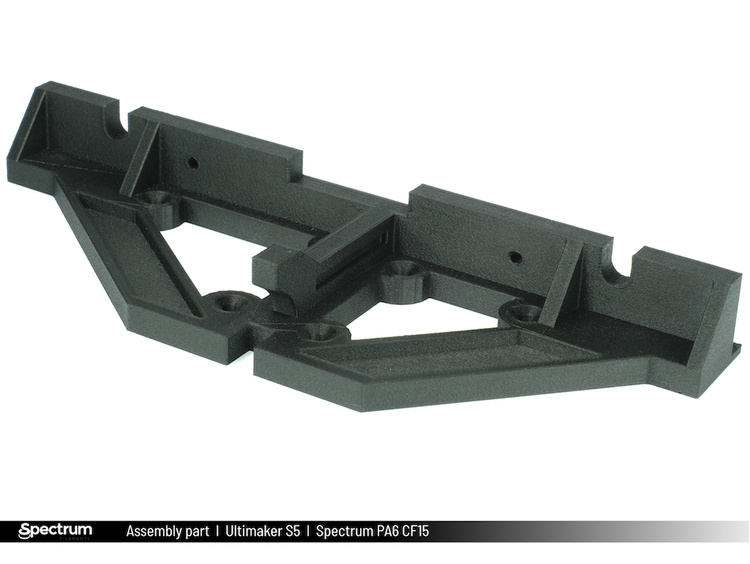

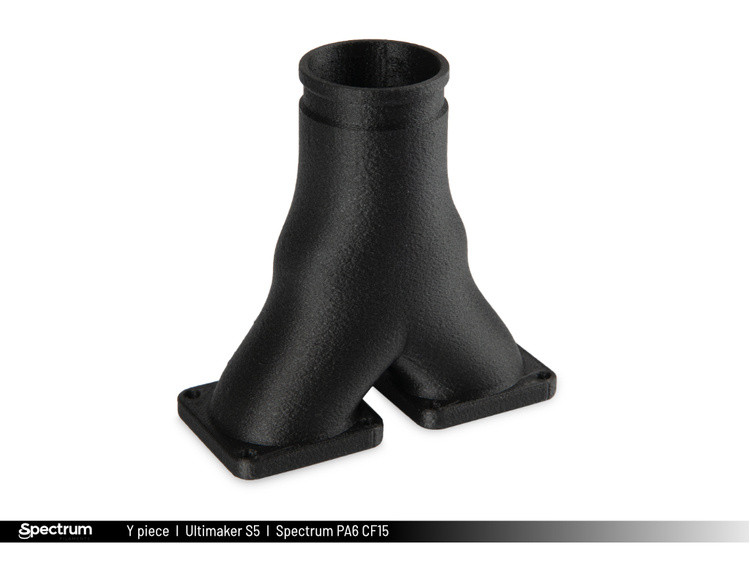
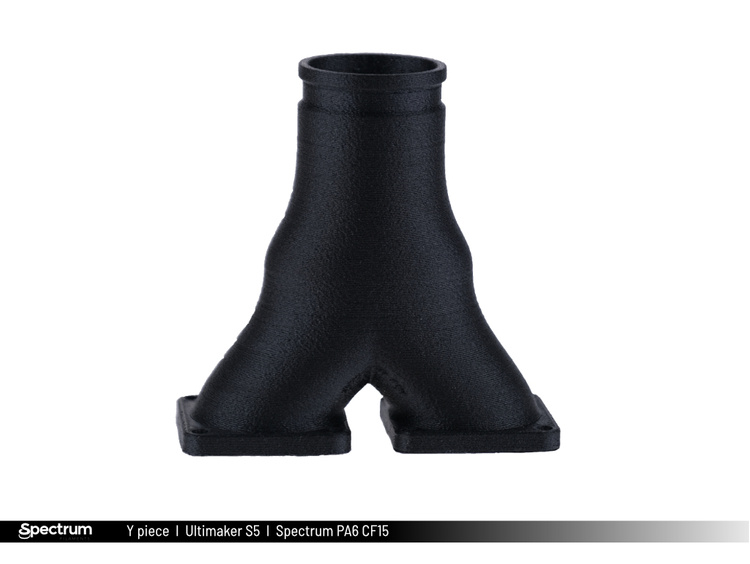


Filament Spectrum PA6 CF15 1.75mm BLACK 0.75kg

High-temperature engineering filament Spectrum PA6 CF15 with 15% carbon fibre content for maximum strength, stiffness and thermal resistance.
✔️ Diameter 1.75 mm, spool 0.75 kg
✔️ Thermal resistance up to 150 °C long-term and 180 °C short-term
✔️ Extremely low shrinkage (~0.1%) and dimensional stability
✔️ Reinforced with 15% chopped carbon fibres
✔️ Lower moisture absorption and faster drying than pure PA6
✔️ Printing without the need for a heated chamber
✔️ Hardened or ruby nozzles 0.5 mm+ recommended
✔️ Ideal for functional parts, gears and industrial prototypes Show more
High-temperature engineering filament Spectrum PA6 CF15 with 15% carbon fibre content for maximum strength, stiffness and thermal resistance.
✔️ Diameter 1.75 mm, spool 0.75 kg
✔️ Thermal resistance up to 150 °C long-term and 180 °C short-term
✔️ Extremely low shrinkage (~0.1%) and dimensional stability
✔️ Reinforced with 15% chopped carbon fibres
✔️ Lower moisture absorption and faster drying than pure PA6
✔️ Printing without the need for a heated chamber
✔️ Hardened or ruby nozzles 0.5 mm+ recommended
✔️ Ideal for functional parts, gears and industrial prototypes Show more
Spectrum PA6 CF15 filament is a high-temperature engineering material based on polyamide 6 reinforced with 15% chopped carbon fibres. It offers exceptional mechanical strength, stiffness and thermal resistance with very low shrinkage, making it an ideal choice for industrial applications and functional parts.
Key features
Adding carbon fibres to the PA6 matrix fundamentally improves both the mechanical and thermal properties of the material. The filament achieves exceptionally low linear shrinkage (down to 0.1%), a high heat deflection temperature (HDT A 200 °C according to ISO 75) and a low coefficient of thermal expansion (0.4 × 10⁻⁵/K). Parts made from this material can withstand long-term operation at temperatures up to 150 °C (up to 20,000 h) and short-term up to 180 °C (max. 200 h). Compared to pure PA6, it has half the moisture absorption and a four times faster drying time. The material excels in high resistance to abrasion and creep, and offers very robust interlayer lamination. Printing does not require a heated chamber and no significant warping of prints occurs. The material is compatible with HIPS and PVOH support filaments.
Printing parameters
| Parameter | Value |
|---|---|
| Nozzle temperature | 270-290 °C |
| Bed temperature | 90-105 °C |
| Print speed | 30-60 mm/s |
| Recommended layer height | 0.15-0.25 mm |
| Recommended nozzle diameter | 0.5 mm and above (hardened steel / ruby) |
| Enclosed chamber | Not required |
| Cooling | Off or minimal |
| Drying before printing | 80 °C / 6-8 hours |
| Linear shrinkage | ~0.1% |
| Water absorption | below 0.3% (23 °C / 24 h) |
Who is Spectrum PA6 CF15 filament suitable for
The material is intended for professional users, designers and industrial applications where a combination of high mechanical strength, thermal resistance and dimensional stability is required. Typical uses include the production of gears, racks and guide rollers operating at elevated temperatures, ring and plate seals with increased chemical resistance, functional prototypes, end-use parts, tooling and industrial modelling. Thanks to the reinforcement with carbon fibres, it is also suitable for parts subjected to wear and high loads.
Printing tips
- Always dry the material thoroughly before printing (80 °C for 6-8 hours) - polyamide is highly hygroscopic.
- Store in a dry and dark place with humidity below 15%, ideally in a sealed box with silica gel.
- Due to the abrasive content of carbon fibres, use hardened steel or ruby nozzles.
- It is recommended to use a nozzle with a diameter larger than the standard 0.4 mm - ideally 0.5 mm or more.
- Keep model cooling to a minimum or turn it off completely for better interlayer adhesion.
- An enclosed chamber is not mandatory, but preventing drafts improves print quality and layer adhesion.
- For maximum mechanical strength, use a slower print speed and a higher nozzle temperature within the recommended range.